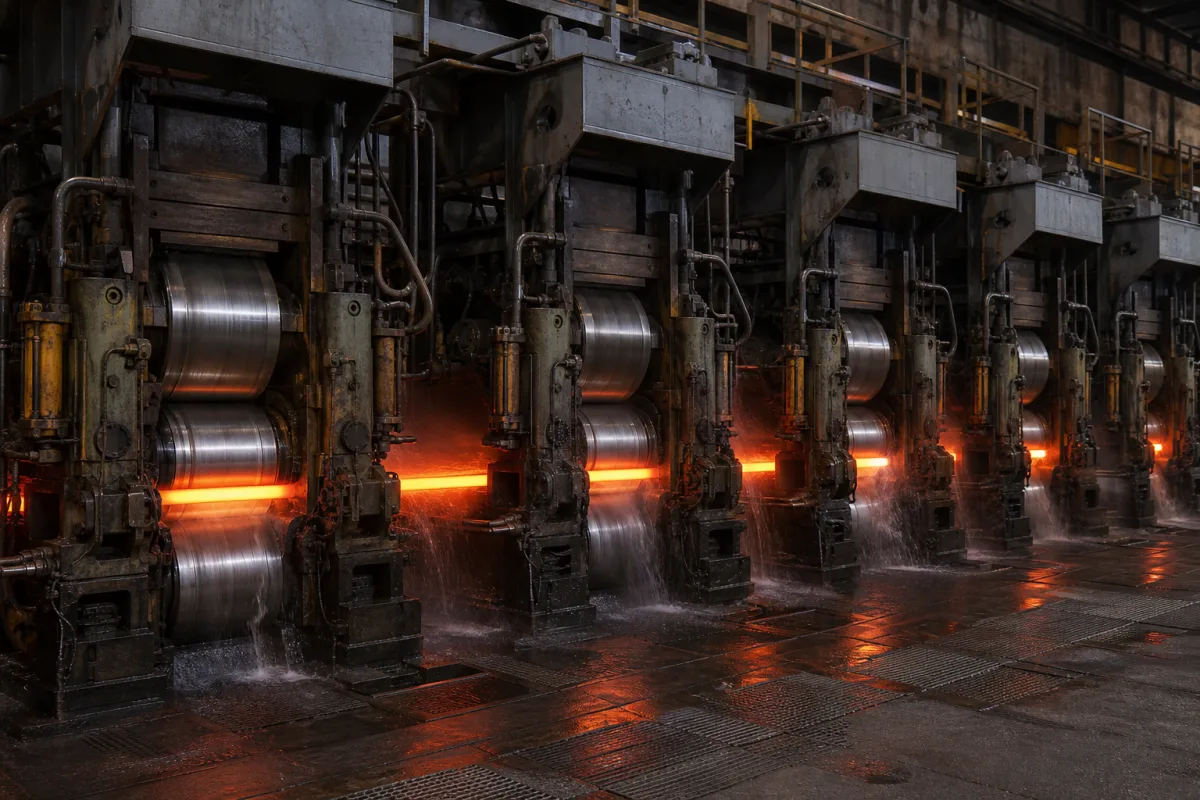
技术参数与制造背景: 精轧机组
| 参数 | 典型区间 | 选型说明与越界后果 |
|---|---|---|
| 机架数量 | 5–7 支架 | Determines reduction capability and final thickness range. |
| 轧辊直径 | 600–800 mm | Affects roll strength and strip shape control. |
| 辊身长度 | 1200–2000 mm | Determines maximum strip width. |
| 最大轧制力 | 20000–40000 kN | Limits thickness reduction per stand. |
| 带钢宽度范围 | 600–1600 mm | Defines product envelope. |
| 出口厚度范围 | 1.2–12.7 mm | Final product thickness after finishing. |
| 最大轧制速度 | 1200–1500 m/min | Affects productivity and cooling control. |
| 厚度公差 | ±0.05 mm | Tighter tolerance improves downstream processing.ASTM A568 |
| 宽度公差 | ±1.0 mm | Critical for edge trimming and slitting.ASTM A568 |
| 表面粗糙度 (Ra) | 0.5–2.0 µm | Affects paintability and forming.ISO 4287 |
| 主传动功率 | 5000–10000 kW | Determines acceleration and torque capability. |
| 工作温度 | 800–1000 °C | Strip temperature at entry to finishing mill. |
| 冷却水流量 | 500–1000 m³/h | Required for roll cooling and strip cooling. |
| 设备重量 | 500–1000 t | Foundation design and installation logistics. |
区间为行业参考值,供询价时圈定范围用,不构成供应商承诺。下单前请向法人制造商核实每一项数值与标准。
| pressure: | 每机架高达3000千牛(典型轧制力) |
| flow rate: | 未提供 |
| temperature: | 600-1200°C(热轧温度范围) |
诱因 → 失效模式 → 工程缓解
不是客户评论,也不是实时热度。以下维度用于前期 RFQ 准备和供应商评估。
这些项目是采购核对事项,不代表真实客户评分、具体国家买家反馈或实时询盘。
说明目标数量、应用场景、交期和关键技术要求,用于准备 RFQ 或供应商评估。
参考参数中,机架数量通常为5至7个。具体数量取决于轧机设计和产品要求。
轧辊通常由合金钢或碳化钨制成,如材料列表所示。选择取决于耐磨性和成本考虑。
厚度公差为±0.05毫米,依据ASTM A568。这是参考值,实际公差可能随操作条件变化,必须与制造商确认。
带钢入口温度通常在800°C至1000°C之间。该范围对于实现所需的冶金性能和轧制性能至关重要。
CNFX 是开放目录,不是交易平台或采购代理。工厂资料和表单用于帮助你准备直接沟通。
CNFX 制造商资料、技术分类、公开产品信息和持续合理性检查。